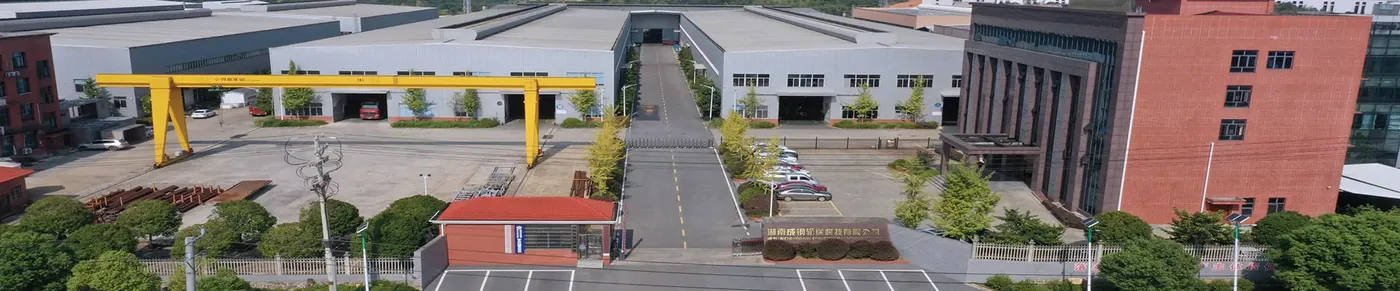
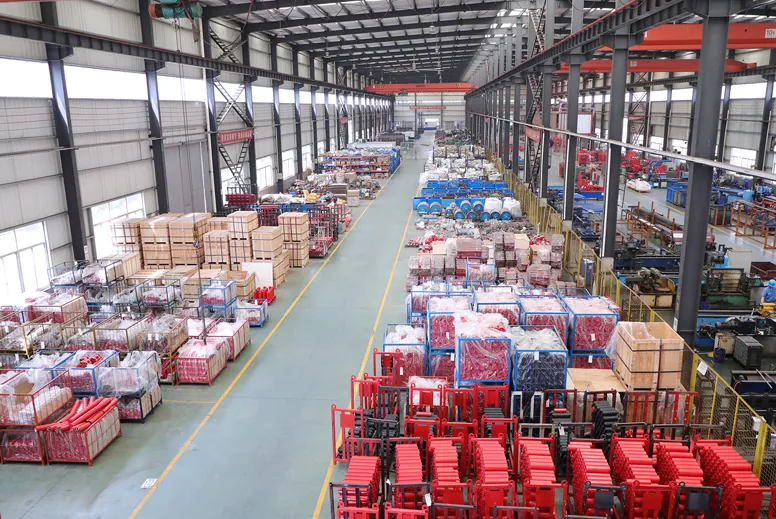
Tube cutting, shaft machining, bearing assembly, welding, coating and final inspection all happen in-house. That is why we can hold a tolerance, trace a defect to a batch, and commit to a delivery date without hedging.
A conveyor idler looks simple. Its service life is decided by four things we control in-house: tube concentricity, shaft accuracy, weld integrity and seal design.
Micron-level accuracy on tube length and squareness — the first determinant of runout and belt tracking.
Slot and end machining on roller shafts for consistent bearing seating and end-cap retention.
Pulley and shaft turning to exact tolerances, so lagging and bearing fits stay concentric under load.
Displacement-robot welding gives uniform, high-strength welds on rollers and pulleys, batch after batch.
Surface preparation before coating — the difference between paint that lasts a season and paint that lasts years.
Anti-corrosion finishing in zinc, epoxy or powder, applied on a dedicated high-temperature line.
Bearing, seal and retention-cap assembly on dedicated lines for repeatable torque and grease fill.
Rotational resistance, runout, dust/water ingress and dimensional checks before a unit is tagged.
Export packing matched to container loading and long-distance handling.
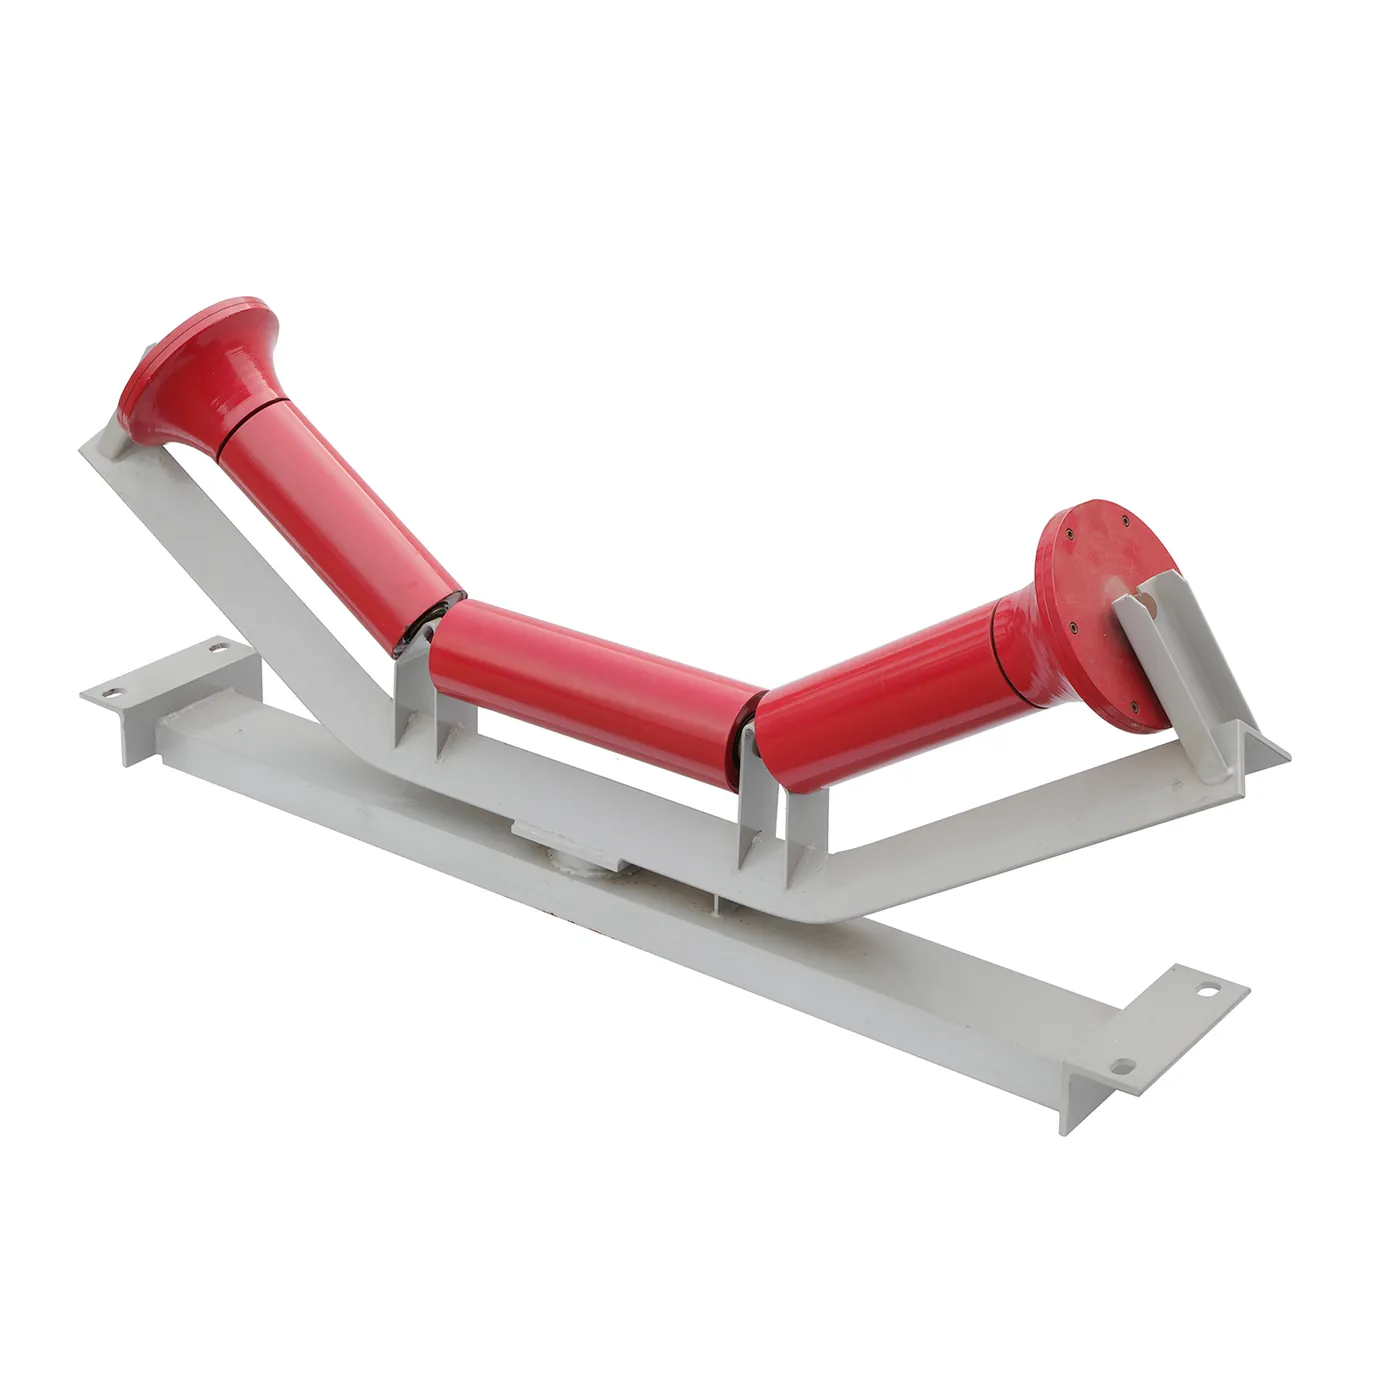
Automated roller assembly with in-line inspection.
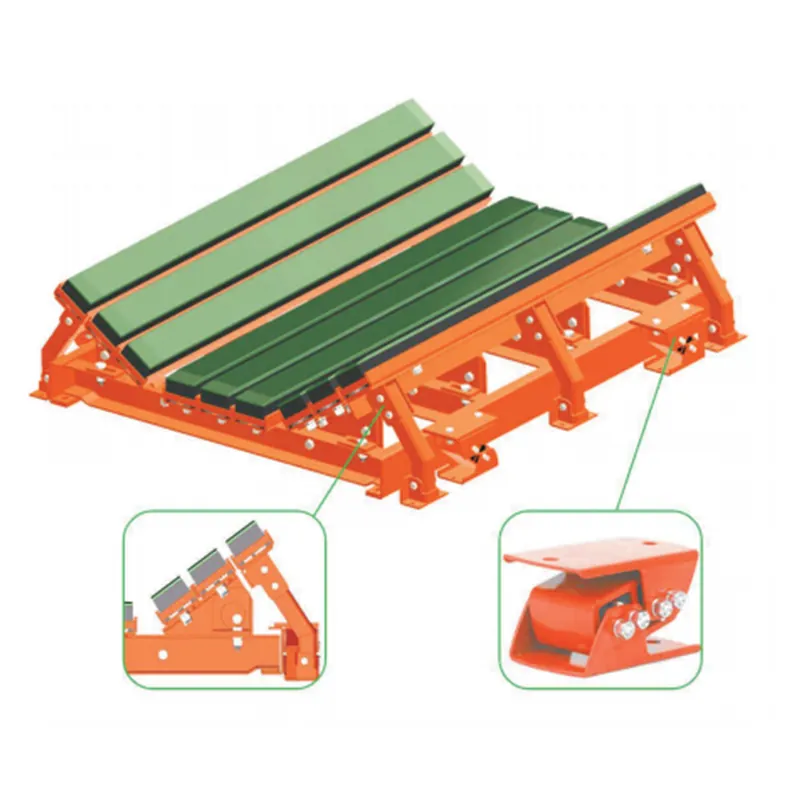
CNC turning and shaft preparation.
Robot welding for rollers and pulley shells.
Dimensional and rotational testing before tagging.
Galvanizing, electrostatic and baking finish options.
Staging and export packing by order and container.
We run inspection from incoming steel tube through to final rotational testing. Every unit carries a unique ID, so if a batch ever underperforms we can trace it back to material, machine and operator.
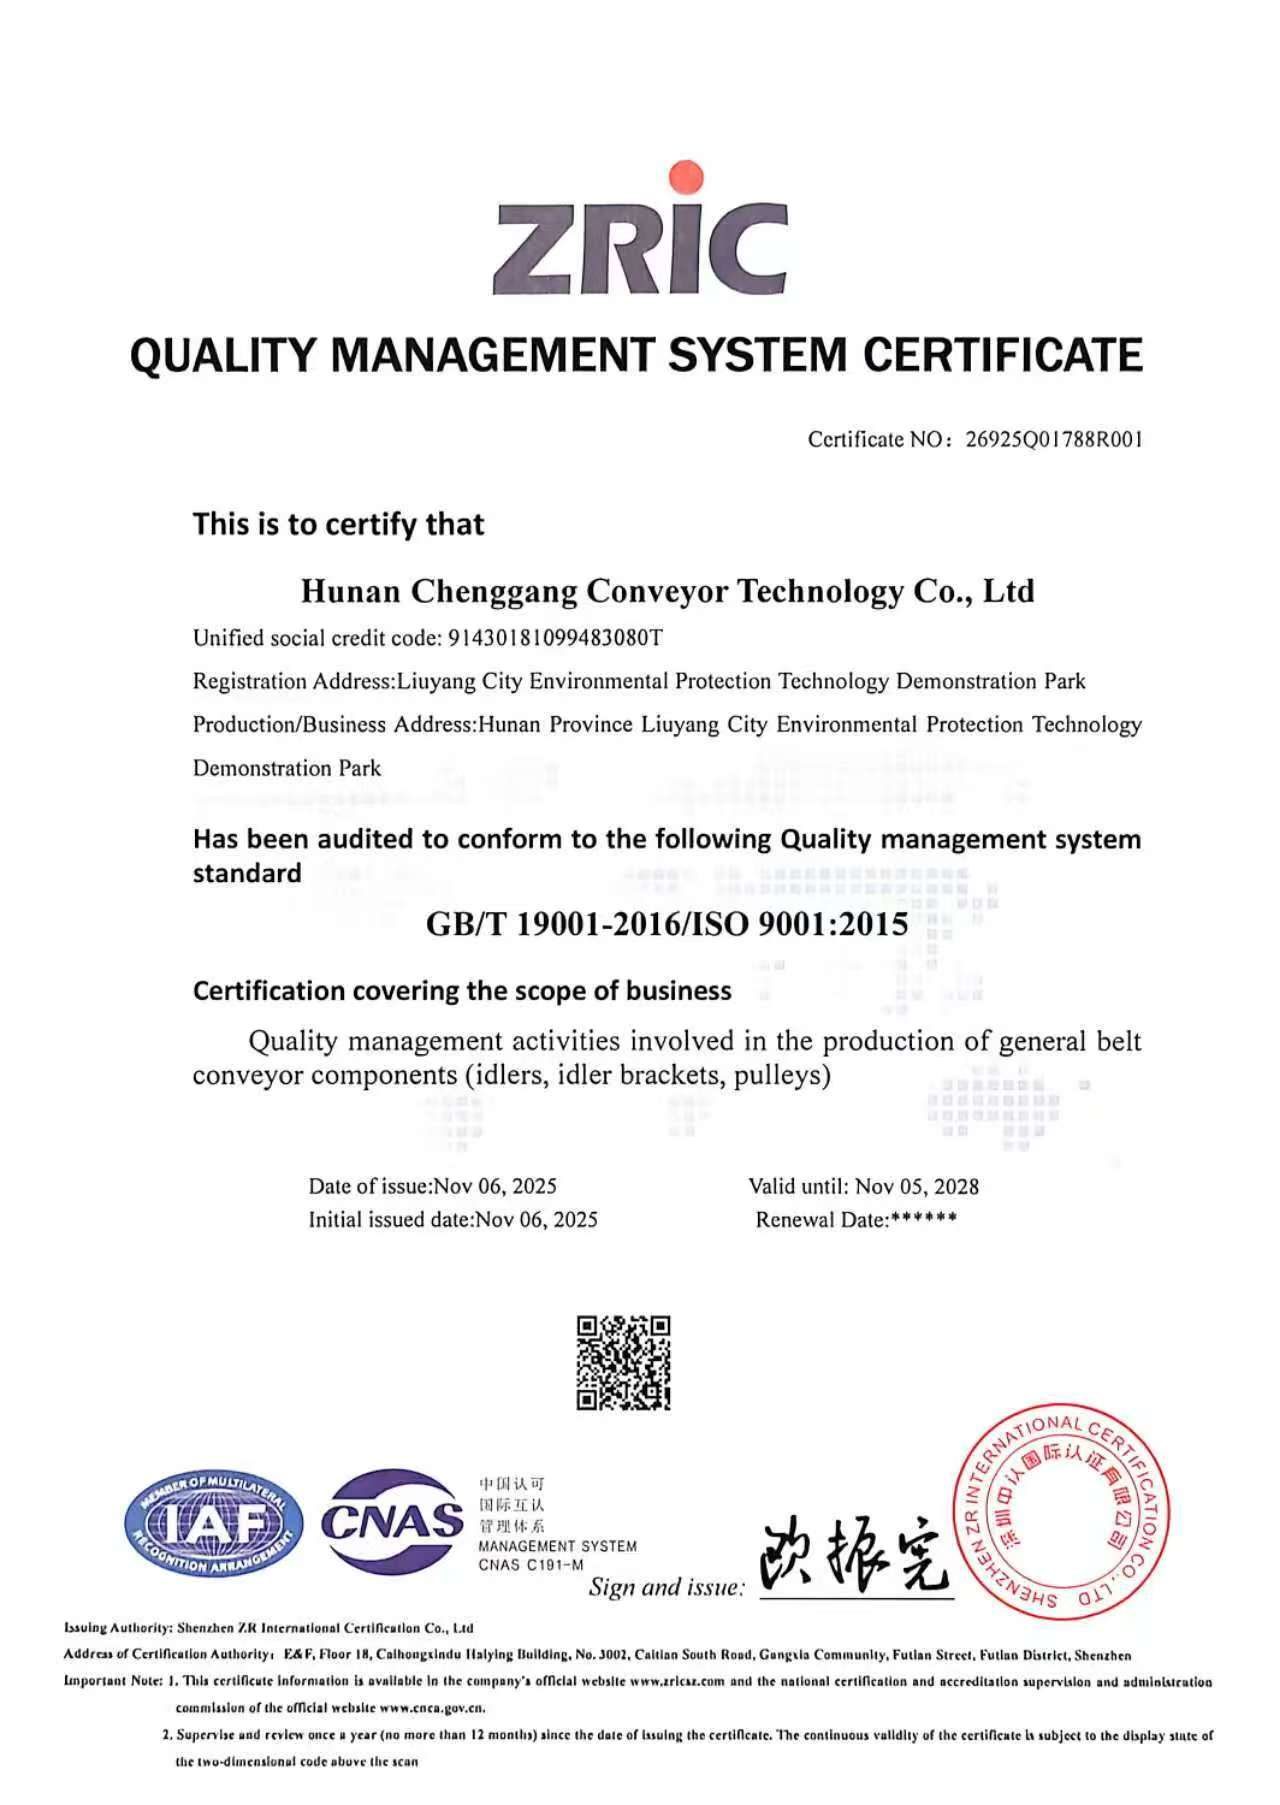
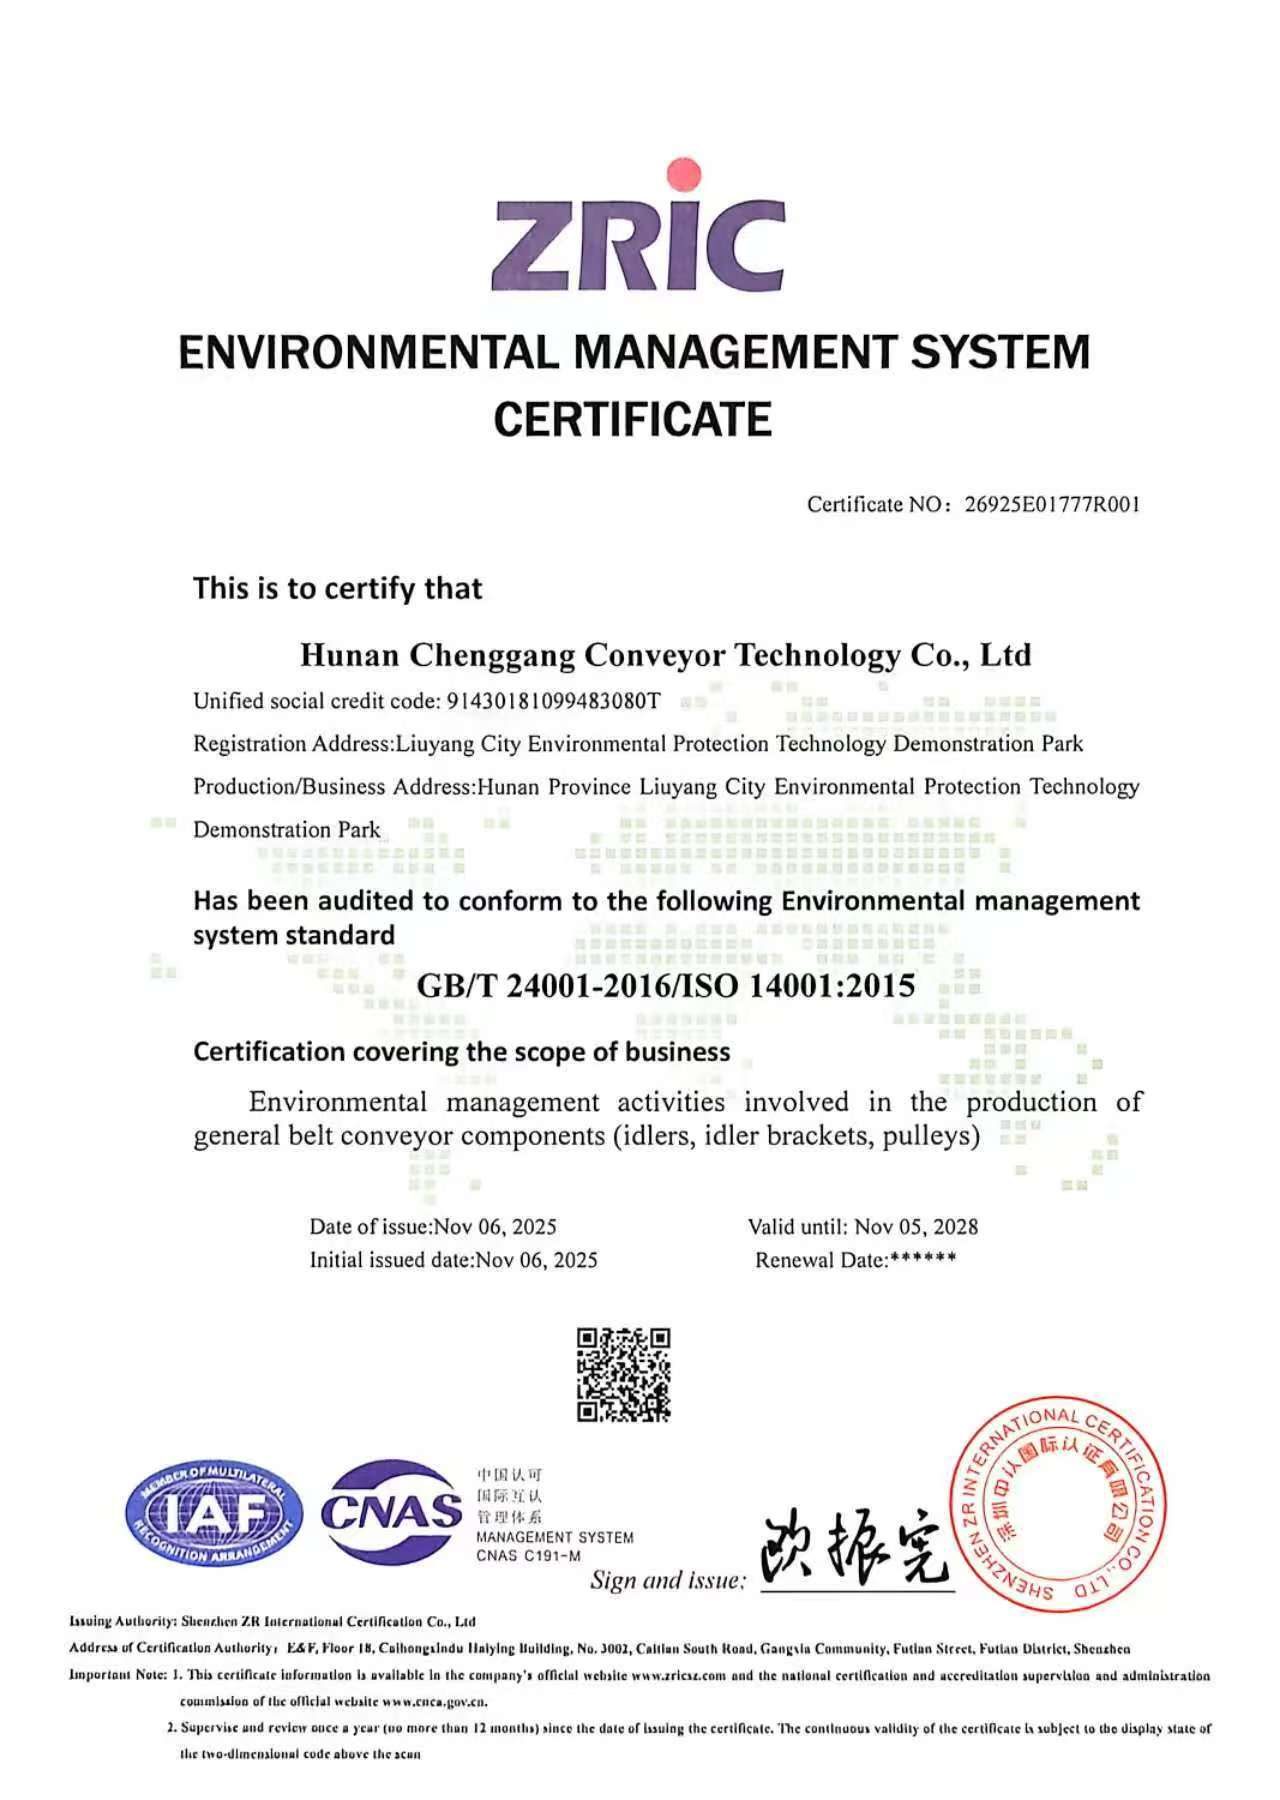
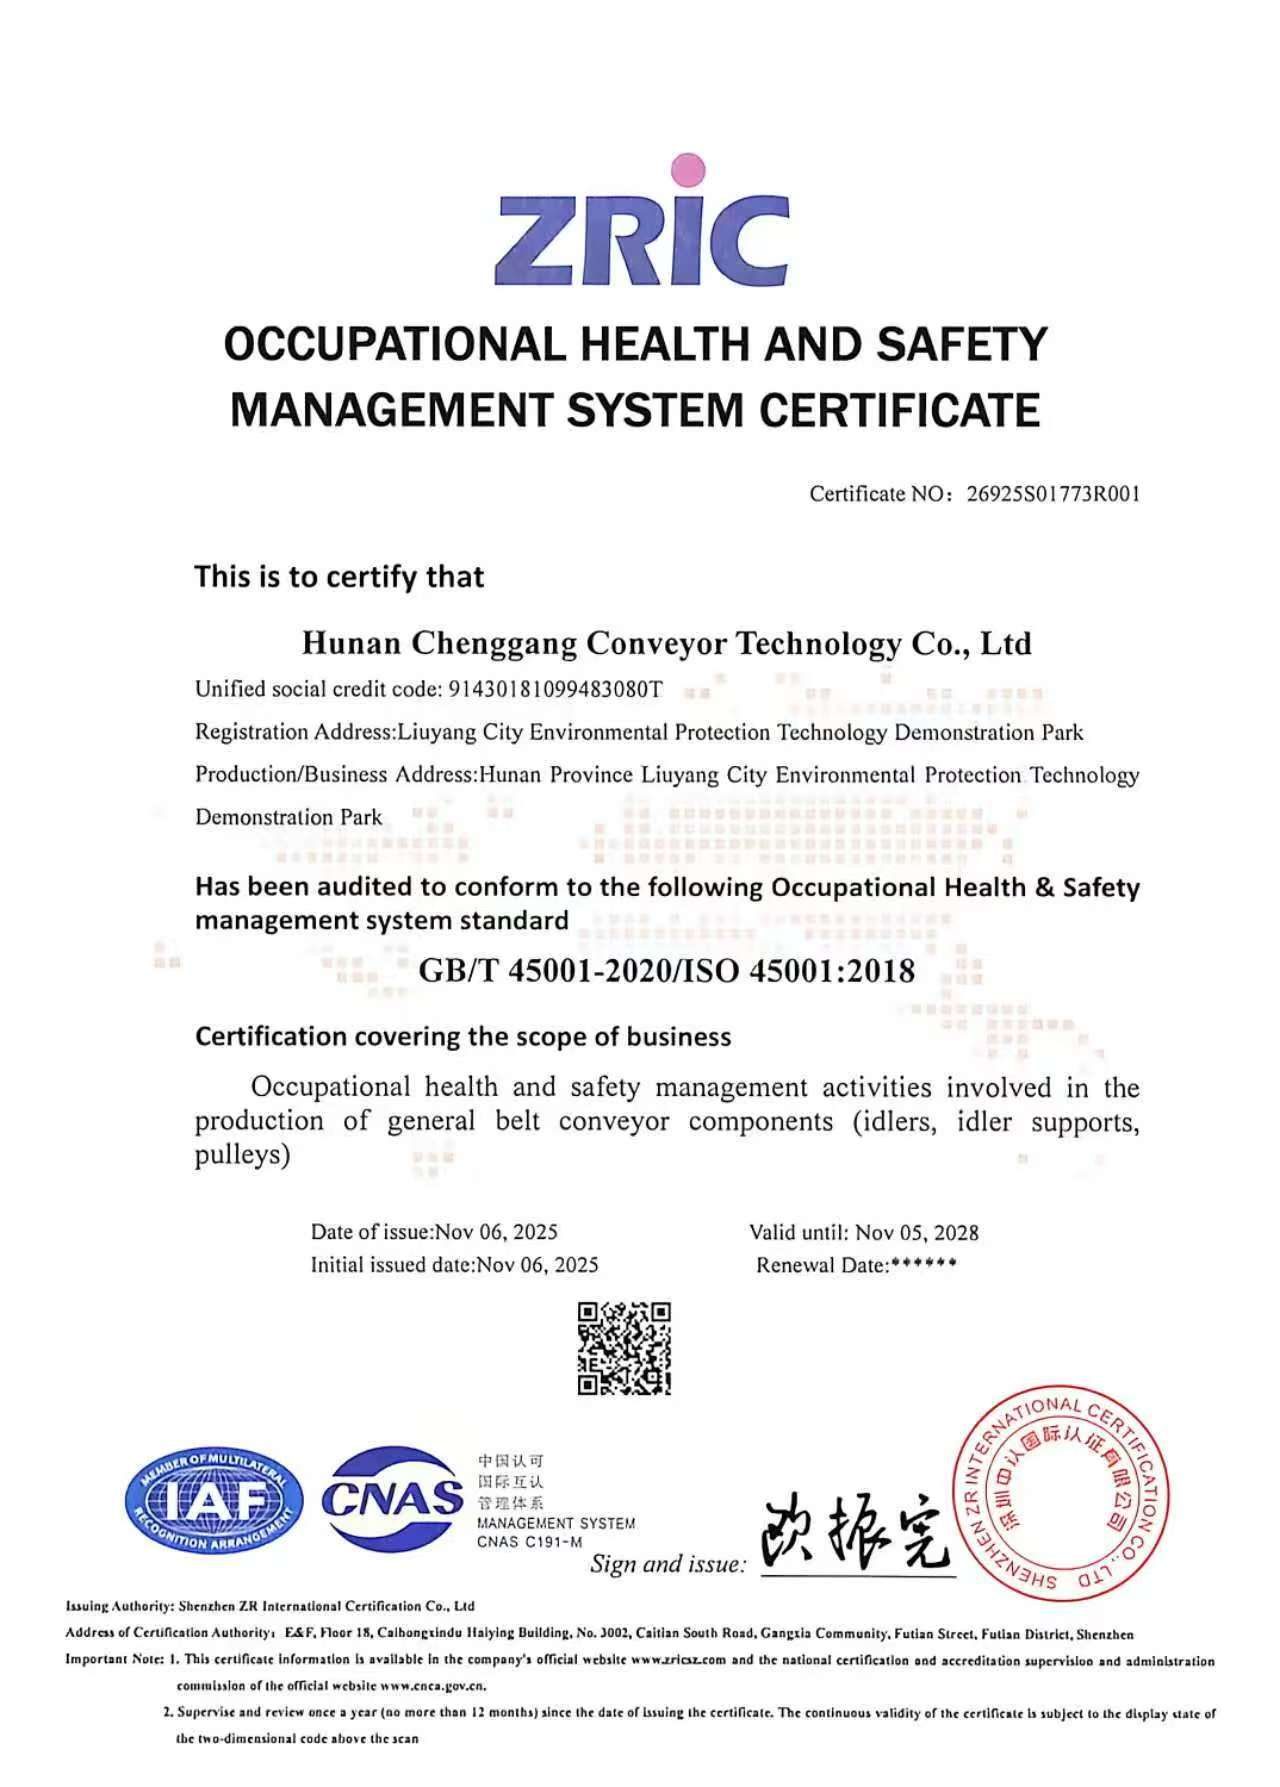
Issued by ZRIC (Shenzhen Zhongren International Certification), a CNAS-accredited body. The scope covers the production of belt conveyor components — idlers, idler brackets and pulleys. Every certificate number above is publicly verifiable with the issuing body. 7 patents and 100+ industry honours.
We can arrange a live video walk-through of the workshop, or host you on site in Liuyang. Bring your drawing — we will review it with the production team on the call.
Book a Factory Tour